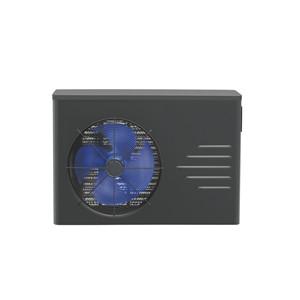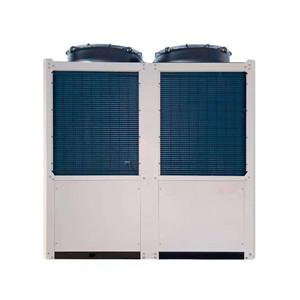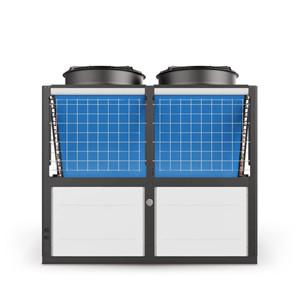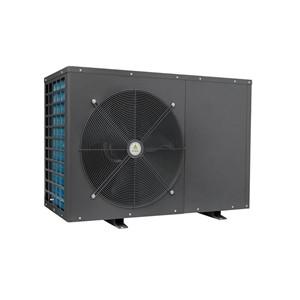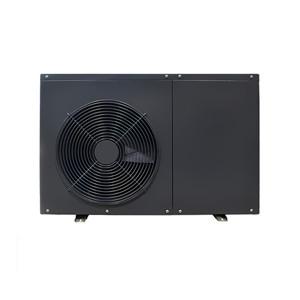
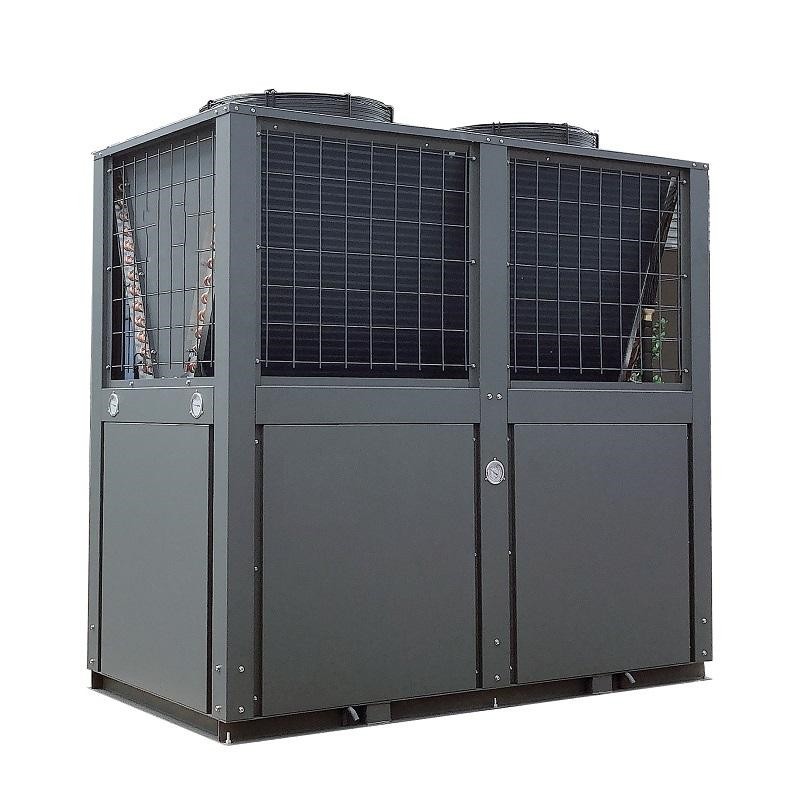
Description
Leveraging Leomon’s EVI technology, variable-frequency technology, the use of the specialized refrigerant R1233zd, and expert calibration, Leomon heat pumps deliver outlet water temperatures of up to 120°C, even in cold weather.
The 120°C high-temperature heat pump represents a remarkable technological innovation, offering a wide range of applications and distinct advantages.
Capable of producing hot water up to 120°C with low operating costs, this system ensures the smooth continuity of production processes. It meets the high-temperature water requirements of industries such as slaughterhouses, electroplating plants, textile printing and dyeing facilities, chemical manufacturing, pharmaceuticals, and aquaculture.
Features
* Uses R1233zd, an eco-friendly refrigerant with low Global Warming Potential (GWP).
* Hot water temperature range: 60°C to 120°C.
* Features DC inverter technology for quiet operation.
* High energy efficiency (COP of 3.5 to 5.5).
* Multiple protection functions.
* Compact structure for easy installation.
Advantages
1. Two-stage cascade technology suitable for extremely cold climates
The unit employs two-stage compression technology with independent low-temperature and high-temperature circulation systems. Even when the ambient temperature drops to -35°C, the system intelligently adjusts the operation of both stages to maintain a stable 120°C hot water output. Dual compressors operate alternately to balance operating pressure and prevent overload. This technology effectively resolves the common issue of single-stage heat pumps shutting down due to excessive compression ratios in extreme cold.
2. Significant energy savings and low operating costs
Compared to traditional electric boilers, this cascade heat pump offers substantial savings on energy costs. It extracts heat from the ambient air and uses two-stage compression to heat water to 120°C, generating far more thermal energy than the electrical energy consumed. The unit requires smaller transformers and power lines than electric boilers, thereby reducing initial investment costs. Most industrial users can recoup their investment in a short period through reduced energy bills.
3. Intelligent Control and Remote Monitoring System
The unit features an advanced, proprietary microcomputer control board capable of automatic operation, scheduled start/stop, intelligent zone-based defrosting, and precise temperature control via a dual-circuit system. It rapidly acquires operating parameters and issues control commands to ensure stable performance. Users can monitor real-time data and status, remotely control power and temperature settings, and receive alarm notifications via a mobile app. Engineers can perform remote fault analysis and diagnostics, thereby enhancing service efficiency.
4. Safe, Clean, and Eco-friendly
The unit operates without combustion, open flames, or emissions, eliminating risks associated with gas leaks, explosions, or carbon monoxide poisoning. It produces clean steam free from boiler chemicals or combustion residues, making it an ideal choice for industries with strict safety and hygiene standards. The use of eco-friendly refrigerants further minimizes impact on the ozone layer and reduces greenhouse gas emissions.
Applications:
* Industrial Manufacturing: High-temperature hot water for production operations and process heating.
* Food Processing: Hot water for production, cleaning, heating, and related processes.
* Slaughterhouses: Hot water for cleaning, processing, and disinfection.
* Electroplating: Temperature control and heating for electroplating processes.
* Chemical Industry: Process fluid heating and industrial hot water supply.
* Commercial Buildings: High-temperature hot water and space heating systems.
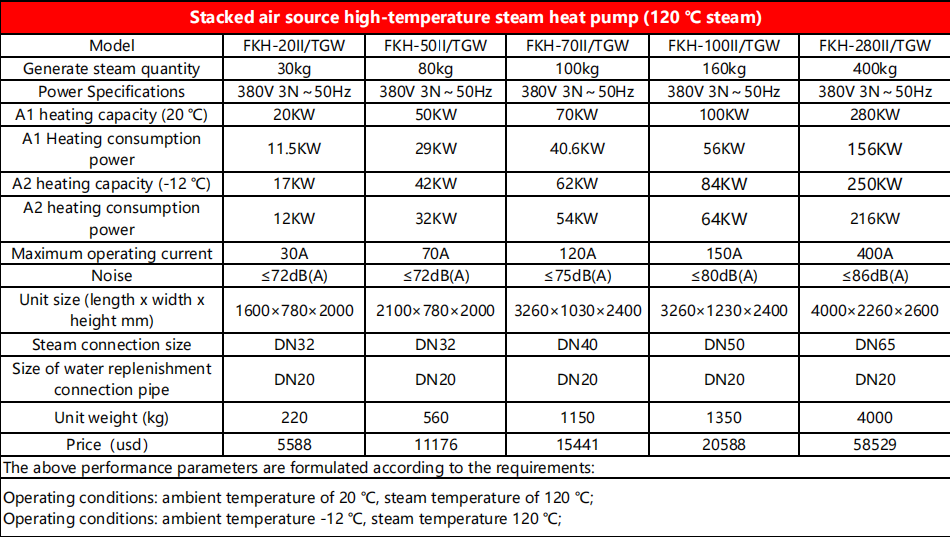
Specifications:
Get Further Assistance
Please contact us for the best high-temperature hot water solutions.