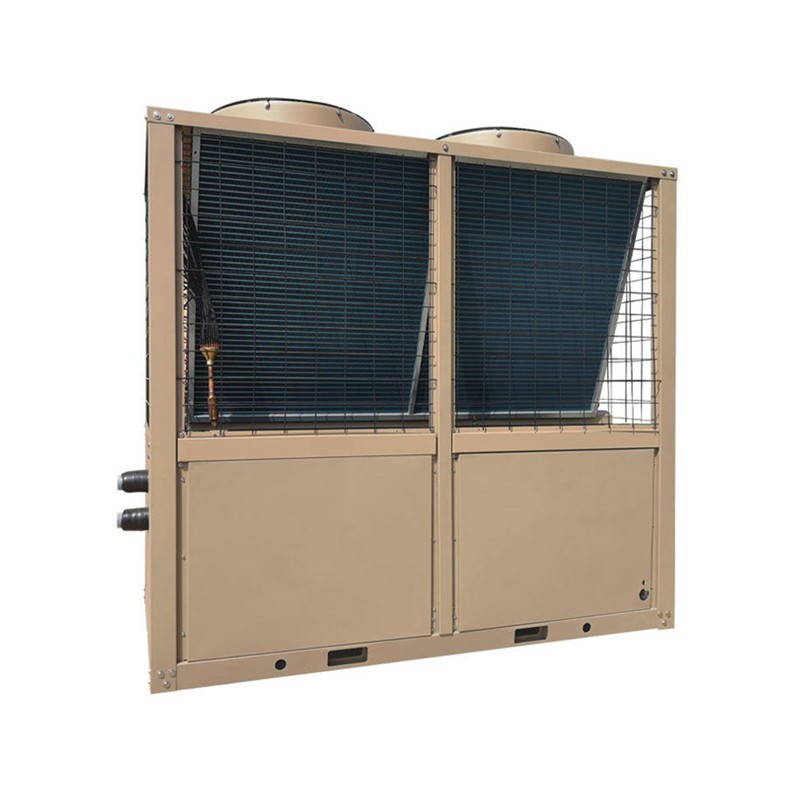
Description
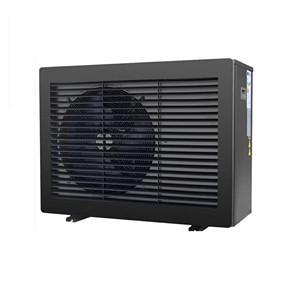
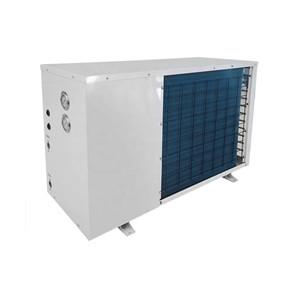
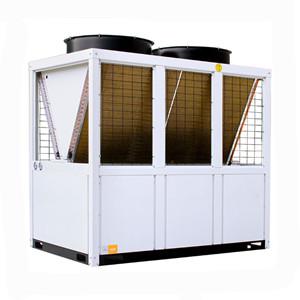
The 120°C high-temperature steam heat pump is an industrial steam generation unit specifically designed for process heating. It primarily generates 120°C saturated steam, providing stable steam temperature and pressure for various industrial processes.
By absorbing low-grade heat from ambient air and utilizing a reverse Carnot cycle to upgrade the thermal energy, the heat pump achieves significant energy savings—reducing energy consumption by up to 80% compared to traditional electric or oil-fired boilers.
Featuring a corrosion-resistant structure, intelligent PLC control, and multiple safety protection functions, this unit operates efficiently at ambient temperatures as low as 15°C. It is widely used in industries such as food processing, chemicals, textiles, pharmaceuticals, and papermaking.
Advantages
1. High-Capacity Output for Centralized Steam Systems
Centralized steam supply systems require reliable sources to meet the combined demands of multiple production lines, process units, and plant heating systems. This unit delivers the high-capacity steam output required for these applications, generating sufficient 150°C saturated steam to support full-plant operations. It maintains stable pressure and temperature even during peak production periods when multiple steam-consuming units operate simultaneously, ensuring uninterrupted production.
2. Significant Energy Savings Compared to Traditional Boilers
Industrial steam generation is often one of the largest energy consumers in manufacturing plants. By absorbing heat from ambient air and converting it into high-temperature steam, the heat pump produces thermal energy far exceeding the electrical energy consumed. Energy savings are substantial compared to resistance-type electric boilers and even more significant when compared to gas or coal-fired boilers. An intelligent control system optimizes performance based on real-time demand, minimizing energy waste and maximizing efficiency.
3. Clean, Oil-Free Steam for Sensitive Processes
The unit generates steam through heat transfer rather than combustion, producing steam that is clean, oil-free, and additive-free. It eliminates the need for boiler chemicals and produces no combustion residues or contaminants that could compromise product quality. This high-purity steam is crucial for industries such as food processing and pharmaceuticals, where product quality and contamination control are paramount. A closed-loop system ensures consistent steam quality throughout the distribution network.
4. Modular Design with Scalable Capacity
The equipment features a modular design, allowing production capacity to expand in line with growth. Facilities can start with a single unit and incrementally add modules as steam demand rises, thereby spreading out investment costs. This modular design also offers installation flexibility; units can be arranged according to available space and configured to meet specific steam distribution requirements.
Applications
1. Large-Scale Food Processing Plants
Food processing plants require steam for various processes, including cooking, sterilization, drying, blanching, and cleaning. This equipment delivers high volumes of steam to support diverse operations across multiple production lines. The clean, oil-free steam ensures food remains uncontaminated and complies with food safety standards. It is suitable for a wide range of food processing facilities.
2. Chemical Manufacturing Complexes
Chemical plants require steam for reactor heating, distillation columns, reboilers, heat tracing, and process heating. This unit provides a continuous, reliable steam supply essential for chemical production. Its corrosion-resistant construction withstands harsh chemical environments, while zero-emission operation eliminates pollution risks. It is suitable for petrochemicals, fine chemicals, and specialty materials production.
3. Pharmaceutical Parks
Pharmaceutical manufacturing requires clean steam for sterilization-in-place (SIP), equipment sterilization, and process heating. This unit delivers the pure, oil-free steam required for pharmaceutical applications and maintains steam quality throughout the distribution network. It is suitable for facilities producing active pharmaceutical ingredients (APIs), sterile injectables, vaccines, and biological products.
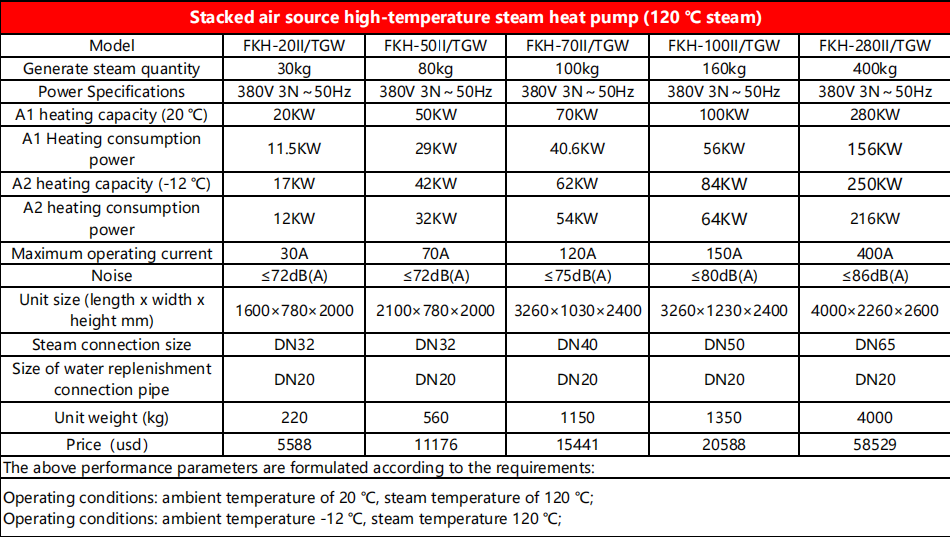
Specifications:
Get Further Assistance
Please contact us for the best high-temperature hot water solutions.